Precision Injection Mold Repair & Reconditioning Services
Rapid-response injection mold repair, micro-laser welding, parting line reconditioning, and core-cavity rework to eliminate flashing, restore SPI Class tooling precision, and minimize press downtime.
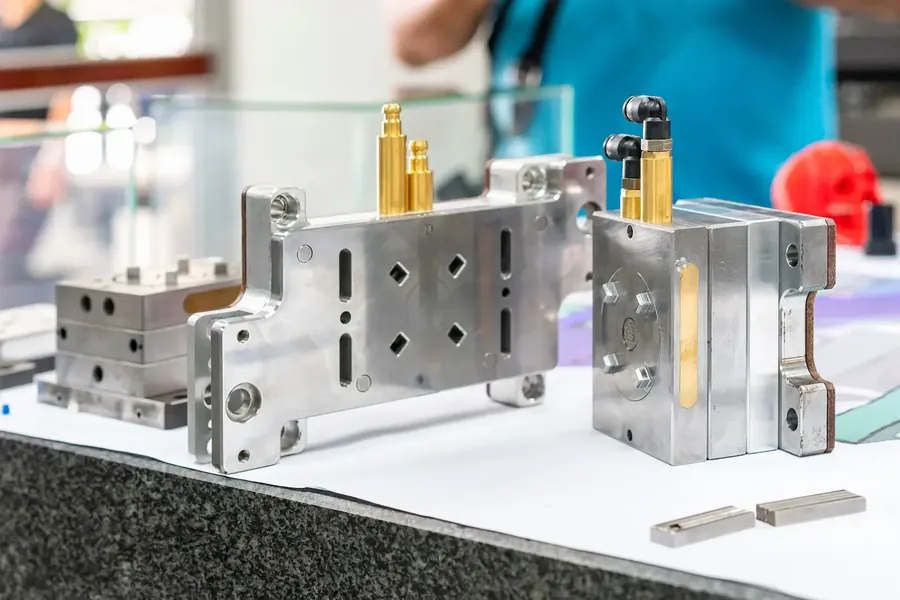
Protecting Production Cycles with Engineering-Led Mold Repair
From critical parting line damage to complex core-cavity fatigue, our certified toolmakers combine advanced laser deposition, CNC hard milling, and sinker EDM to return your molds to factory-spec tolerances.
Unplanned injection mold downtime can halt entire production schedules and cost tens of thousands of dollars per day. At Engineering Innovation, our specialized mold repair facility provides rapid-turnaround diagnostics, metallurgical remediation, and preventive overhauls for automotive, medical, industrial, and consumer plastic injection molds.
Whether your mold has suffered accidental clamp collisions, gate erosion, severe parting line flashing, or seized ejector pins, we avoid aggressive grinding that alters part wall thicknesses. Instead, we use state-of-the-art fiber laser deposition welding to add precise tool steel only where needed, followed by 5-axis hard milling up to 60 HRC to restore exact dimensional integrity.
Comprehensive Injection Mold Restoration & Overhaul
High-precision corrective and preventive maintenance services across single-cavity prototypes and multi-cavity Class 101 high-production tooling.
Parting Line Restoration & Flash Elimination
Crushed shut-off surfaces and worn parting line edges cause severe plastic flash. We restore mating edges using low-heat laser deposition and blue-spotting hand bench fitting to achieve 100% shut-off contact.
- Zero plastic flashing
- Spotting press contact validation
- Re-machined draft angles
- No loss of cavity volume
Core & Cavity Micro-Laser Welding
Cracked, chipped, or eroded cavity walls repaired with precision pulsed fiber laser welding. Low heat input prevents metallurgical annealing, warping, or heat-affected zone (HAZ) embrittlement.
- Matched alloy wires (H13, S7, P20, 420 SS)
- Zero thermal distortion
- Hardness matching up to 54 HRC
- Sub-millimeter weld bead control
Ejector System & Slider Overhaul
Galled, bent, or seized ejector pins and mechanical side-action sliders cause part deformation and press alarms. We ream worn guide bushings, replace angle pins, and re-machine hardened slider wear plates.
- Oversized precision ejector pin fitting
- Graphite-plugged bronze wear plate replacement
- Hydraulic core-pull cylinder servicing
- Stroke and alignment calibration
Cooling Line Descaling & Leak Repair
Scale buildup, clogged baffles, and internal water leaks cause unequal cooling, long cycle times, and part warpage. We chemically descale circuits, replace damaged O-rings, and hydrostatically test up to 10 Bar.
- Chemical ultrasonic descaling
- High-pressure 10 Bar leak testing
- Bubbler and baffle replacement
- Corrosion remediation
Sinker EDM & Texture Re-Graining
Fine rib damage, narrow slot repair, and surface finish restoration using multi-axis CNC sinker EDM. We re-spark damaged geometries and blend cosmetic textures to match SPI polish or Mold-Tech standards.
- Sub-micron CNC sinker EDM rework
- Mold-Tech texture matching
- SPI A-1 diamond mirror polishing
- Gate and runner profile optimization
Hot Runner Manifold Servicing
Complete electrical, thermal, and hydraulic service for valve-gate and open-tip hot runner manifolds. We resolve internal plastic seepage, replace burnt heater bands, and recalibrate thermocouples.
- Plastic freeze and purge cleanout
- Valve pin and bush reconditioning
- Thermocouple continuity validation
- Balanced thermal profile verification
Book Precision Tooling Rework
24/48h Emergency Fast-Track • Micro-Laser Welding (Zero HAZ)
Common Mold Failure Modes We Permanently Fix
We do not just patch the symptom; our engineering team diagnoses the root mechanical, thermal, or rheological cause to prevent recurring failures.
Flash on Parting Line
Ejector Pin Galling & Seizure
Gate Washout & Cavity Pitting
Internal Cooling Water Leaks
Engineered Mold Repair Workflow
A repeatable, transparent process ensuring your production mold returns to service with full dimensional inspection reports.
Teardown, Ultrasonic Cleaning & CMM Inspection
Complete disassembly of plates, slides, and manifolds. Ultrasonic degreasing followed by 3D optical scanning and CMM measurement against master CAD to pinpoint wear.
- Ultrasonic deep cleaning
- 3D scan wear map generation
- Spotting bluing evaluation
- Root cause diagnostic report
Micro-Laser Welding & Deposition
State-of-the-art pulsed fiber laser welding builds up damaged shut-offs, core tips, and cavity surfaces using metallurgical matching wire, eliminating thermal distortion.
- Argon-shielded micro-welding
- Base steel hardness verification
- Minimal HAZ heat dissipation
- Pre-weld metallurgical inspection
High-Speed CNC Milling, EDM & Polishing
High-speed hard milling up to 58 HRC and sinker EDM recreate original CAD geometries. Experienced bench toolmakers hand-polish and stone surfaces to SPI specifications.
- High-speed 5-axis hard milling
- CNC sinker EDM spark erosion
- Diamond stone bench finishing
- Mold-Tech texture blending
Kinematic Fit, Pressure Testing & Final QC
Full bench reassembly, spotting press alignment, 10 Bar water manifold pressure testing, and slider kinematic checks. Signed CMM inspection certificate provided.
- Blue-paste shut-off spotting check
- 10 Bar cooling pressure test
- Ejector & slider stroke verification
- Full CMM inspection certificate
Tooling Tolerances & Metallurgical Specifications
Our repair tolerances match or exceed original European and US moldmaking industry standards.
| Feature | Standard Repair Tolerance | High-Precision Tooling Spec | Verification Method |
|---|---|---|---|
| Parting Line Shut-Off Flatness | ±0.015 mm | ±0.005 mm (0.0002 in) | Blue-Paste Spotting & Dial Indicator |
| Core & Cavity Dimensional Accuracy | ±0.020 mm | ±0.008 mm | 3D Laser CMM Scanning |
| Weld Hardness Retention | 48 - 52 HRC | 54 - 58 HRC (Through-Hardened) | Equotip Micro-Hardness Tester |
| Cooling Line Hydrostatic Pressure | 6 Bar (87 PSI) | 10 Bar (145 PSI) | Hydrostatic Pressure Gauge (30 Min) |
| Surface Finish Restored | Ra 0.8 µm (SPI B-2) | Ra 0.025 µm (SPI A-1 Diamond) | Optical Profilometer |
Frequently Asked Questions About Injection Mold Repair
Straightforward answers from our tooling engineering team regarding timelines, costs, and repair procedures.
Connected Repair, Reconditioning & Tooling Services
Explore our complete suite of industrial machinery repair, precision tooling reconditioning, and replacement component manufacturing.
Industrial Machinery Repair
Heavy industrial machinery repair, mechanical overhauls, shaft reconditioning, and emergency breakdown support.
CNC Machine Service & Maintenance
Preventive maintenance, spindle alignment, servo drive calibration, and emergency CNC machine repair.
Custom Tooling & Spare Parts
Rapid CNC reverse engineering and fabrication of replacement mold inserts, core pins, and worn tooling components.
Precision CNC Tooling Rework
High-precision 3-axis and 5-axis CNC hard milling and EDM rework for damaged mold plates and steel cavities.
Injection Mold Manufacturing & Overhauls
Full mold re-manufacturing, multi-cavity tool overhauls, and engineering change order (ECO) retrofits.
3D Mold Reverse Engineering & Redesign
3D blue-light optical scanning, digital repair modeling, parting line re-engineering, and Moldflow validation.